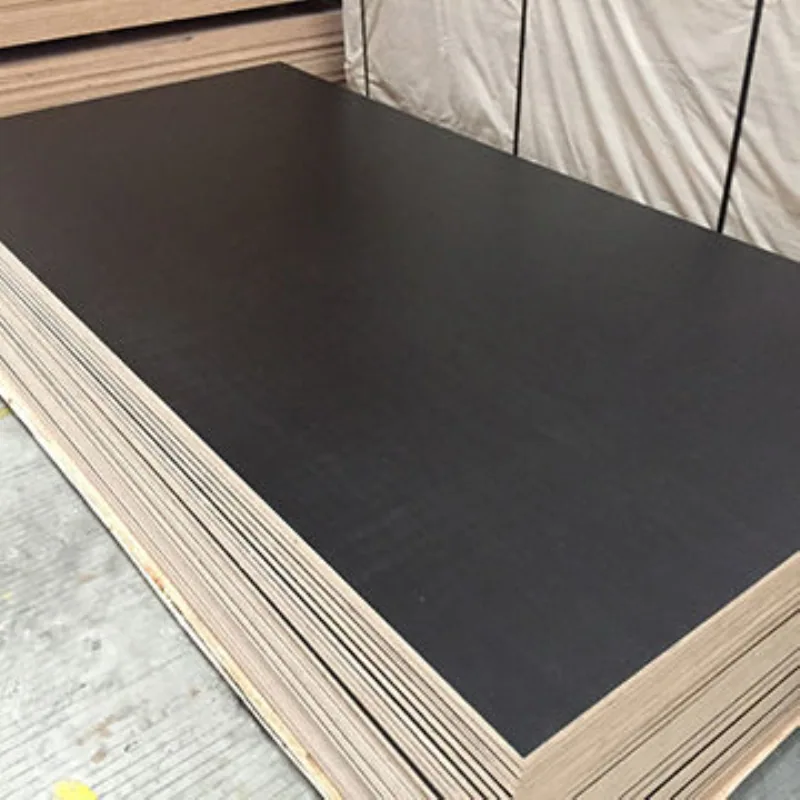
The 12mm panel. The right fit. Ready for your next job.
Get film faced plywood for formwork infill, supported linings, moulds and cut components. Choose your core, WBP bond and working film, then order sheets or factory-prepared parts around your cutting list.
Available to order · 10–15 days production · Container shipping
TECHNICAL DATA · TDS-PS-16 · Rev 2.0 (Oct 2026)
12mm Film Faced Plywood technical data
A 1220 × 2440 × 12mm combi-core sheet weighs about 22.1 kg, with 9 plies and a 620 kg/m³ loading basis. Choose the core, film weight and WBP bond for your formwork facing, lining or factory-cut components.
12mm combi-core weight and loading · 1220 × 2440mm sheet
Construction
12 mm; 9 plies; combi core at 620 kg/m³ for loading
Area and sheet weight
7.44 kg/m²; approximately 22.1 kg per sheet, before export packaging
Estimated 40HQ quantity
~1,212 pcs, using a 26.8-tonne panel allowance
These loading figures apply to the combi-core sheet shown. We prepare the packing plan with your chosen sheet format, bundle dimensions, packaging weight, container limits and delivery route.
Service Class 3 (Severe Exterior & Wet Concrete Pouring Exposure)
Edge Sealing Treatment
2–3 coats waterproof acrylic/PU edge paint, matched brown, black, red or custom RAL colour
Standard Sheet Sizes
1220 × 2440 mm, 1250 × 2500 mm, 1200 × 2400 mm, 1500 × 3000 mm
12mm Thickness Tolerance (2-Time Press)
±0.35 mm (EN 315)
Length & Width Tolerance
±1.0 mm (EN 315)
Moisture Content at Dispatch
8.0 – 12.0% (EN 322)
Squareness (Diagonal Difference)
≤ 1.0 mm / m (EN 324-2)
Edge Straightness
≤ 1.0 mm / m (EN 324-2)
Panel Flatness
≤ 2.0 mm / m (EN 315)
Your quotation brings the selected core, working film, WBP adhesive and finished dimensions together. Send the component size and formwork detail so we can match the 12mm supply to the parts you need.
Compare core, bond and surface properties
Read the technical data with the named core, film weight and test condition. The 620 kg/m³ loading basis above is within the declared combi-core density range. For formwork design, request the panel data for your selected 12mm construction and supporting arrangement.
Core, bond and surface properties in the film-panel technical data sheet
Density (Poplar / Combi / Eucalyptus / Birch Core), kg/m³
530 / 600 / 670 / 700 (±30) Test method: EN 323
Moisture Content at Dispatch, %
8.0 – 12.0 Test method: EN 322
Modulus of Elasticity — Longitudinal (MOE //), MPa
≥ 5,500 (Poplar) / ≥ 7,200 (Eucalyptus/Birch) Test method: EN 310 / GB/T 17656
Modulus of Elasticity — Transverse (MOE T), MPa
≥ 4,200 (Poplar) / ≥ 5,800 (Eucalyptus/Birch) Test method: EN 310 / GB/T 17656
Bonding Shear Strength (72h Boiling — WBP), MPa
≥ 1.0 (No delamination after 72h @ 100°C) Test method: EN 314-2 Class 3
No blistering, softening, or fiber raising Test method: DIN 18215
Thickness Swelling (24h Water Immersion, Sealed), %
≤ 5.0 Test method: EN 317
Product classification and reference standards
Harmonized System (HS) Code
4412.33 / 4412.39
Reference Standards
EN 13986, EN 636-3, EN 314-2 Class 3, BS 5268, AS/NZS 6669, GB/T 17656
Film-panel range: estimated reuse by core and film
Estimated pour reuse cycles for the stated film-panel constructions
Poplar Core
8–12×
Combi Core
12–18×
100% Eucalyptus/Birch + Dynea WBP
20–35+×
These are the estimated ranges for the named constructions in our film-panel data sheet. Plan your 12mm working trial with the selected core, film, release system, support and concrete finish. Cutting, edge protection, stripping, cleaning and storage also affect the panel’s working life.
Other thicknesses, loading quantities and 18mm bending data
Use the following thickness options when comparing the parts for a mixed-thickness order. The 12mm row retains its own 9-ply construction and 22.1 kg sheet weight; each other thickness is a separate configuration.
Series thickness tolerances: 12–18 mm: ±0.35 mm | 21–30 mm: ±0.45 mm (EN 315), for the two-time-pressed calibrated construction.
Weight and loading basis: nominal 1220 × 2440mm sheets, combi-core construction at 620 kg/m³, before export packaging. Approximate 40HQ counts use a 26.8-tonne panel allowance and the rounded sheet weights shown. The packing plan accounts for bundle dimensions, packaging weight and the container and route payload limits.
Series thickness options: combi-core sheet weight and estimated 40HQ loading · 620 kg/m³
Nominal Thickness
Ply Count
Area Weight
Sheet Weight (1220 × 2440mm)
Est. Load / 40HQ
9 mm
7 plies
5.58 kg/m²
16.6 kg
~1,614 pcs
12 mm
9 plies
7.44 kg/m²
22.1 kg
~1,212 pcs
15 mm
11 plies
9.30 kg/m²
27.7 kg
~967 pcs
18 mm
13 plies
11.16 kg/m²
33.2 kg
~807 pcs
21 mm
15 plies
13.02 kg/m²
38.8 kg
~690 pcs
24 mm
17 plies
14.88 kg/m²
44.3 kg
~604 pcs
27 mm
19 plies
16.74 kg/m²
49.8 kg
~538 pcs
30 mm
19 plies
18.60 kg/m²
55.4 kg
~483 pcs
18mm film faced plywood bending reference
These bending values describe the 18mm constructions in the same film-faced range. For your 12mm formwork component, request the relevant core and layup data for the required supporting design.
1830 × 915mm, other requested formats and factory-cut parts
Core options
Poplar, combi, eucalyptus hardwood or birch; other veneer mixes as custom configurations
Working film
Black, brown or red; 120, 135, 180 or 220 g/m² film
WBP adhesive systems
Phenolic WBP or high-melamine WBP, selected for the use and exposure
Weight and ply configuration
1220 × 2440 × 12mm combi core: 9 plies; approximately 22.1kg at 620kg/m³ before packing
Dispatch moisture content
8–12% for the calibrated-core configuration
Sheet geometry
Length and width ±1.0mm; squareness, straightness and flatness listed in technical data
Face and reverse
Specify both working faces, finish and film reference
Factory processing
Full sheets, cut blanks, drilling, edge treatment and labelled component kits
Formwork detail
Carry panel direction, support, fixing and face-level requirements with the component drawing
Order planning
Available to order; normally 10–15 days production; container shipping; 180-day after-sales warranty
Choose the construction, finish and size for your project. We’ll bring the selected options and finished tolerances together in your quotation.
FROM A PANEL SIZE TO A READY-TO-FIT PART
Make your 12mm order work for the way you build.
Need a replacement liner, formwork infill or a repeat set of mould parts? Send the board you use, a photo or your cutting list. We manufacture 12mm film faced plywood and can supply full sheets, cut blanks or machined components with sealed edges and identified packs.
Buy sheets for your workshop
Choose the core and film, then compare the format with the parts you need. Standard sheets include 1220 × 2440, 1250 × 2500, 1200 × 2400 and 1500 × 3000mm. The smaller 1830 × 915mm format is also available as a custom order.
Move repeat preparation into our factory
Send finished sizes, holes, face direction and part quantities. We can include cutting, drilling, edge treatment and kit labels in the quotation, so your team receives parts organised for the next job.
A 1220 × 2440 × 12mm combi-core sheet with 9 plies weighs approximately 22.1kg on the 620kg/m³ loading basis. That gives you a clear starting point for sheet handling; the finished packing list includes the selected core, format and packaging.
CHOOSE THE CORE, BOND AND WORKING FACE
Get the surface you want on the construction you need.
Choose the 12mm core around your work
Core
Useful starting point
Compare in the sample
Poplar
Weight-conscious handling and cost-conscious components
Film, edge condition and finished fit
Combi
General formwork parts and repeat component orders
Veneer layup, machined edges and fixing details
Eucalyptus hardwood
Repeated forming and demanding handling
Film weight, bond and performance in the intended site cycle
Birch
Machined components and system-formwork parts
Finished thickness, joints and cut-edge quality
Film for your finish
Choose black, brown or red film in 120, 135, 180 or 220 g/m² options. Include the working face and reverse in the request. For concrete appearance, compare the film with your release treatment and joint detail on a working panel.
WBP bond for wet work
Our formwork range offers phenolic WBP and high-melamine WBP adhesive systems. Tell us about wet concrete contact, storage and the site cycle so we can recommend the core, bond and film together.
Need another veneer mix or a dry-use industrial liner? Send the contact material and operating conditions. We can quote that construction separately from the WBP formwork range.
INFILL · SUPPORTED LININGS · MOULDS · CUT KITS
Choose the part you want to make.
Formwork infill and closures
Fit gaps and opening surrounds with accurately cut pieces. Include supported edges, the adjacent face level and attachment points so the supplied part fits the form.
Replaceable supported linings
Use a smooth film face over the planned backing. Keep the replacement size and drilling pattern with the part reference to make the next set straightforward to order.
Precast mould parts
Order returns, inserts and shaped components around the concrete finish you need. Review corners, release and stripping with a first working part before repeating the kit.
Curved or profiled faces
Share the curve, panel direction and backing. We help plan a supported forming trial and inspect the film and veneer condition before the production order.
Industrial liners
Describe abrasion, impact, moisture and cleaning contact. We help select the face and core and include cut-outs, fixings and edge protection in the component supply.
Repeated assembly kits
Group parts by assembly, drawing revision and working-face direction. Factory cutting and labelling help your team spend less time sorting and preparing the delivery.
For a formwork face spanning between supports, use the project's loading, panel direction, support and fixing design with the selected 12mm construction. If the design calls for 18mm, compare 18mm Concrete Shuttering Plywood; for a wider choice of panels, see our Film Faced Shuttering Plywood range.
THICKNESS, BACKING AND A FLUSH WORKING FACE
Make the finished panel fit the frame.
The calibrated-core configuration uses 12mm ±0.35mm finished thickness: a band of 11.65–12.35mm. Length and width tolerance is ±1.0mm, with dispatch moisture content of 8–12%. Include any tighter recess, joint or accessory fit in the drawing.
Half an inch is 12.7mm. If your existing component is called half-inch, send its measured thickness or frame detail. The nominal difference from 12mm is 0.7mm, which matters at flush joints, clamps and rebates.
Check the full thickness stack
For a panel seated in a rebate, use face offset = panel thickness + compressed backing thickness − rebate depth. Take readings from the finished film-faced sheet and include the backing layer in the assembly check. This gives the workshop a useful method for setting the final working plane.
A change from nominal 18mm to 12mm removes 6mm from the stack. Review the face level, clamp engagement and support arrangement together with the revised design. Keep the accepted frame detail with the sample and later replacement order.
COMPARE FORMATS BY THE PARTS THEY PRODUCE
A smaller sheet does not always mean less material.
For 295 × 1195mm blanks with the long side following the long sheet side, allow 10mm trim at each outside edge and 3mm between parts. The 1220 × 2440 and 1250 × 2500mm formats each fit eight positions; the custom 1830 × 915mm format fits three.
Read the worked detail and calculations
Fixed-direction 295 × 1195mm blank layouts
Source sheet
Usable rectangle
Columns × rows
Blank positions
1220 × 2440mm
1200 × 2420mm
4 × 2
8
1250 × 2500mm
1230 × 2480mm
4 × 2
8
915 × 1830mm
895 × 1810mm
3 × 1
3
Eight positions on the larger format.Four narrow columns and two lengths fit after the stated trims. The 1250 × 2500mm format also gives eight in this grid.Three positions with little width to spare.The three columns need 891mm within a nominal 895mm usable width. Check the actual minimum usable width.
The small sheet is shown as 915mm across by 1830mm along. Three 295mm parts plus two kerfs need 891mm within the 895mm usable width, leaving 4mm. Include edge cleanup and the minimum usable sheet rectangle when planning that tighter layout.
Keep the working-face direction and final machining allowance with the part list. Send the actual components and we can compare formats or factory-cut supply around the delivered piece count.
SHEET COUNT, WEIGHT AND CONTAINER PLANNING
Plan the purchase around the completed parts.
For 96 of the blanks shown above, the eight-position layouts use 12 source sheets; the three-position layout uses 32. The smaller sheets require 50% more input area than 1220 × 2440mm in this particular layout. Add your spare parts and finishing allowance to the order quantities.
Compare sheet quantities for the 96-part layout
Whole-sheet input for 96 required rectangular blanks
Source sheet
Positions per sheet
Sheets required
Input sheet area
Nominal input volume
1220 × 2440mm
8
12
35.7216m²
0.4286592m³
1250 × 2500mm
8
12
37.5000m²
0.4500000m³
915 × 1830mm
3
32
53.5824m²
0.6429888m³
The 96 blanks total 33.8424m² of face area and 0.4061088m³ at nominal 12mm. Compare the full-sheet input with that finished part requirement; offcuts and saw loss remain within the purchased sheet quantity.
Keep the weight with its core and format
The following figures use the same combi-core, 620kg/m³ planning basis. A nominal 1220 × 2440 × 12mm sheet weighs approximately 22.1kg, with 9 plies. Other cores have their own density and finished sheet weight.
Nominal 12mm combi-core sheet mass at 620kg/m³
Sheet dimensions
One-face area
Nominal volume
Calculated mass
1220 × 2440 × 12mm
2.9768m²
0.0357216m³
22.1kg
1250 × 2500 × 12mm
3.1250m²
0.0375000m³
23.3kg
915 × 1830 × 12mm
1.6744m²
0.0200934m³
12.5kg
At the 22.1kg rounded sheet weight, the technical data gives about 1,212 sheets per 40HQ using a 26.8-tonne panel allowance. Bundle dimensions, packaging and route payload limits are included when preparing the final loading plan.
Our bulk price is expressed per m³. For cut parts, we quote the material, machining and edge treatment together with the finished quantities. That makes it easier to compare workshop cutting with factory-prepared supply.
CUT, DRILL, THEN PROTECT THE NEW EDGES
Receive parts ready for the next operation.
Protect the working face during machining
Use a supported cut and trial the blade, drilling and countersinking on the chosen core and film. Include a narrow edge or fixing detail where the part is most sensitive to breakout, and inspect both sides.
Include edges and holes in the finish
Apply the specified protection after cutting and drilling. Check corners, hole exits and recesses before the frame hides them. Restore protection whenever later trimming exposes the plywood again.
Plan edge and hole treatment for the 96-part layout
Each 295 × 1195mm blank has a perimeter of 2.980m. Across 96 parts that is 286.080m, giving 3.432960m² of outside edge area at nominal 12mm. For four 20mm through-holes per part, the 384 hole walls add about 0.289529m².
Treatment boundaries for 96 cut 12mm parts
Boundary
Quantity basis
Nominal exposed area
Outside rectangular edges
96 × 2.980m = 286.080m
3.432960m²
Four 20mm through-holes per part
384 holes × π × 0.020m × 0.012m
Approximately 0.289529m²
Combined boundary area
Outside edges plus hole walls
Approximately 3.722489m²
These dimensions describe the cutting layout, not coating consumption. Plan the treatment quantity with the coating instructions, absorption, application losses and number of coats.
We can supply cut sizes, holes, sealed boundaries and labelled component sets. Add the drawing revision and any assembly groups so your team can receive and use the parts in order.
FROM VENEER TO FINISHED FILM-FACED PANELS
See the production steps behind your order.
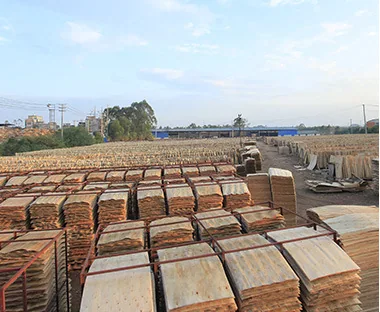
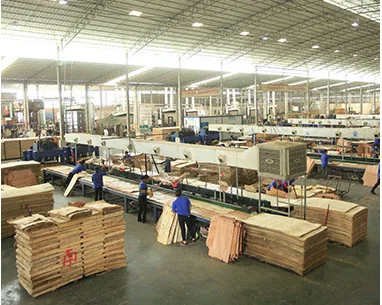
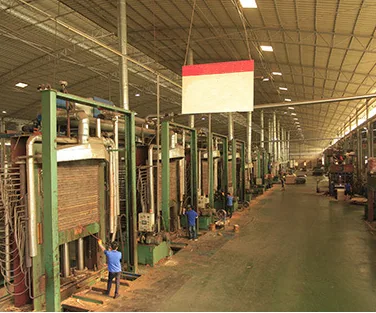
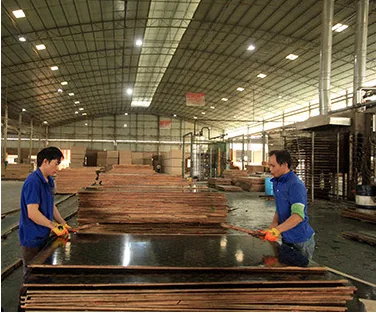
These photographs show veneer preparation, assembly, pressing and finished-panel handling in our film-faced plywood range. Your order carries the selected core, adhesive, film and finished dimensions through these stages.
Veneer preparation before panel assembly.
Prepare the veneer
Condition and arrange the veneers for the selected layup. Material preparation supports consistent assembly, pressing and finished dimensions.
Adhesive at the veneer surface before panel assembly.
Apply the selected adhesive
Match the adhesive system with the core and intended exposure. Application and pressing follow the chosen production process.
Veneer assembly and panel preparation in our workshop.
Assemble the layup
Build the specified construction and keep the order reference with the batch. Check core joints and the regions that will become cut edges or fixing zones.
Panel pressing equipment in the manufacturing sequence.
Press, calibrate and face
Bring the bonded core to the finished thickness, then apply the working film. Inspect completed panels after the facing process.
Handling and checking the finished film-faced panel.
Check and prepare for packing
Inspect dimensions, the film and edge condition. For processed parts, repeat the relevant checks after machining and protection.
SEE THE FACE · CHECK THE FIT · TRY THE PART
Choose a sample that helps you make the decision.
A face-and-core piece
Compare the film colour, reverse and cut edge. Add a machined edge or hole if that detail affects the part you want to order.
A first component or working panel
Check the actual frame, joint and fixing detail. For concrete work, use the planned release system and review both the concrete finish and the panel after stripping.
Keep the selected sample and drawing revision for the production order. Not sure which core or film to request? Send the board you use and tell us what you want to improve: finish, fit, handling or cutting yield.
CHECK THE FINISHED SHEET AND THE SUPPLIED PART
Make receiving easier with clear order records.
What to record for your 12mm order
Check
Order reference
Useful record
Material identity
Core, WBP bond and films on each face
Product and batch reference
Finished dimensions
12mm ±0.35mm and the specified sheet or part size
Measurement positions and readings
Working face and cut core
Chosen film, sample and critical fixing zones
Surface and cut-edge photos
Machining and protection
Drawing revision, holes and edge finish
Finished-part checks after processing
Delivery quantity
Sheets, parts, spares and assembly groups
Pack labels, quantities and loading photos
For a machined component, include checks after sawing, drilling and edge treatment. Keep the selected sample, drawing revision, measurements and pack photos together so the receiving team can identify the material and count the parts.
TECHNICAL DATA AND ORDER DOCUMENTS
Give your purchasing team the information it needs.
Request the 12mm technical data with the core, film, adhesive and dimensions for your order. We can help arrange the relevant product documents, production checks and packing records around the project requirement.
Product data for the chosen construction
Use the 12mm configuration and its weight basis with the quotation. If your project calls for a particular test or declaration, send the requirement so the document pack follows the board you plan to buy.
Plan dimensional readings, surface checks, part counts and pack identification with the order. Review our factory's inspection process before setting the shipment checklist.
Support sheets on level bearers and protect faces, edges and corners during handling. For component kits, keep part numbers, working-face direction and drawing revisions on the pack list; group spares separately from the installation sets.
After use, clean the film with suitable tools, inspect fixing areas and restore damaged edge protection before the next cycle. Retain the chosen construction and sample reference when reordering replacement panels.
Production is arranged to order, normally in 10–15 days, with container shipping. Send the quantity and destination for the packing and freight quotation. Our ordering guidance covers samples, delivery and the 180-day after-sales warranty.
PLAN YOUR PANEL ORDER
Bring the panel and the finished part into one order.
Share what you are making and the dimensions you have. We help choose the construction, arrange a useful sample and quote the finished supply.
Standard samples without special work or a logo have no sample charge; delivery is separate. Custom samples are agreed individually.
Order quantity
Our starting guidance is one container for standard sizes and 3,000–10,000 pieces for custom sizes or designs. Tell us your trial quantity.
Production
All products are made to customer order. Production takes 10–15 days; the order confirmation records the start date and production schedule. Sea transit is additional.
Payment
Where a deposit applies, our standard reference is 30% before production, with the balance after inspection and before loading. T/T or L/C terms are agreed for the order.
Shipping
Panel orders ship by container. Share your destination so we can arrange the loading plan and quote the freight separately from production.
After-sales warranty
All products include a 180-day after-sales warranty. Contact our team with the order reference and details of any product concern.
Tell us your quantity, sample needs and target delivery date. We’ll put the price, payment terms and production schedule into your quotation.
Share the material, thickness and test standard your project requires. Our factory team will help you select the product reports and documents for your purchase.
Production & inspection
We can plan production and inspection around your panel specification, with dimensional checks, recorded readings and packing photographs for your order.
We prepare packing details, pack quantities and dispatch documents for your order. Share the destination and receiving requirements so our team can help plan delivery.
Standard formats are 1220 × 2440, 1250 × 2500, 1200 × 2400 and 1500 × 3000mm. Choose poplar, combi, eucalyptus hardwood or birch. We also offer the custom 1830 × 915mm format and factory-cut parts.
How much does a 12mm sheet weigh?
A nominal 1220 × 2440 × 12mm combi-core sheet weighs about 22.1kg on the 620kg/m³ loading basis, with 9 plies. The technical data uses approximately 1,212 sheets per 40HQ before final packing and route checks. Other sizes and cores have their own weights.
What thickness tolerance should I plan for?
The calibrated-core configuration is 12mm ±0.35mm, giving 11.65–12.35mm. Use the completed film-faced sheet and backing dimensions when planning a flush frame fit. Send any tighter fitting requirement with your drawing.
Is 12mm the same as half-inch plywood?
Half an inch is 12.7mm. Send the metric thickness or measured frame detail for a replacement part so the finished panel fits the rebate, clamp and neighbouring face.
Can 12mm film faced plywood replace an 18mm panel?
We can help plan a 12mm component around your revised design. Review support, loading, fixings and face level together: the nominal thickness change is 6mm. For an existing 18mm formwork requirement, compare our 18mm concrete shuttering range.
Which film and adhesive can I choose for wet formwork?
Black, brown and red film are available in 120, 135, 180 and 220 g/m² options. The formwork range offers phenolic WBP and high-melamine WBP bonds. Include the wet concrete exposure, working faces and reuse plan so we can recommend the construction.
Can you supply cut and labelled parts?
Yes. Send the cutting list, holes, working-face direction, edge treatment and quantities. We can quote full sheets, blanks or processed component kits, with part numbers and drawing revisions on the packing information.
Which sample should I request?
A face-and-core piece helps compare the surface and cut edge. A machined component checks the fixing or frame detail; a working panel helps review concrete appearance and the intended site process. We can arrange the sample around your next buying decision.
Can I get production and inspection documents?
Yes. Send the core, film, dimensions and project document requirement. We help organise technical data, relevant product documents, dimensional checks, part counts and packing records for your order.
How do I request a quote and plan delivery?
Start with the application, panel or part sizes, quantity and destination. Production is arranged to order, normally in 10–15 days, with container shipment. Freight terms follow the order and our 180-day after-sales warranty applies.
Standard sheet sizes: 1220 × 2440, 1250 × 2500, 1200 × 2400 and 1500 × 3000mm
Custom formats: 1830 × 915mm, other requested formats and factory-cut parts
Email a photo, component drawing, formwork detail or previous sample reference to sales@plywoodsupplier.cn. Start with the details you have; we’ll help you work through the rest.
CONTINUE YOUR PANEL SELECTION
Formwork surfaces and concrete finish
Compare our panels
Browse the material range and compare the configurations for your order.
Optional Google Analytics and Ads cookies measure visits and enquiries. Reject keeps these cookies off; basic cookieless measurement continues. Enquiry details are never sent to Google. Privacy details.