
Hot pressing forms the MDF core; cooling and sanding bring it to the thickness and surface your workshop receives. For painted fronts, routed parts and panels to be veneered, these stages influence the material exposed by machining and the preparation needed next. We manufacture MDF substrates in our own factory and help select the supplied board around your component.
Start with the part, a finish photo or a current board sample. We help translate the fit and surface you need into a specification for plain MDF or a faced panel, then plan a useful trial.
Plain MDF specifications Furniture melamine MDF Natural veneer MDF
How hot pressing forms the board
Pressure brings the fibre structure into the required consolidated form while heat enables the binder system to develop its bond. Moisture and temperature vary within the material as the cycle progresses. The outcome depends on the fibre, binder, mat and process combination rather than a single best temperature.
The European Panel Federation's MDF description identifies hot pressing as part of dry-process fibreboard manufacture and distinguishes multi-daylight and continuous routes. These are process types, not guarantees of a particular board's strength or surface quality.
Read pressure, temperature and time on the right basis
| Variable | Record | Keep separate from |
|---|---|---|
| Temperature | Measurement location and actual operating condition | Assuming the heating-system display equals core temperature |
| Pressure | Whether it is hydraulic pressure or pressure on the mat | Unlabeled machine settings from another press |
| Thickness or gap | Control position and the material state at measurement | The cooled and sanded final thickness |
| Time | Dwell, residence or complete cycle, as applicable | Loading and unloading time or a generic seconds-per-millimetre figure |
| Mat moisture | Measurement point, basis and material identity | Moisture reported at another upstream stage |
| Press output | Time, position and board or run reference | An untraceable sample selected later from a mixed stack |
These definitions make records comparable. Equipment and material procedures establish the operating conditions; the finished board is then checked against the order requirements.
Compare batch time and continuous residence
For a batch press, distinguish closing, the relevant pressing stages and opening from the overall cycle. For a continuous press, position along the pressing path and line speed help describe the material's residence. A time value without those definitions can lead to a false comparison.
As an arithmetic example, material moving at a constant 0.5 m/s takes 20 seconds to travel through a 10 m section. This hypothetical transit calculation does not represent a curing prescription or the temperature reached by the core. Stops, speed changes and the thermal behaviour still need their own records.
Compare productivity at the required thickness and quality, using the quantity of usable board. A faster run provides value when the resulting material still meets the specified use.
Look through the thickness as well as at average density
Average density describes mass per volume. The distribution through the thickness describes where that mass is concentrated. Boards with similar averages can therefore behave differently when routed, bonded, bent or fixed near an edge.
Research on process-related variation across an HDF production line examines density and mechanical variation in a specific industrial setting. It illustrates the need to retain sampling position. Its HDF results should not be converted into universal acceptance limits for MDF.
For a deep routed front, compare the exposed core and the face after finishing. For a bonded panel, also check the relevant surface and internal-bond requirements. A process change can affect those properties differently, so the component helps determine which results to review.
Trace splits and blisters to the process history
A split, blister or weak internal plane after pressing can have several contributing factors. Review the mat condition, binder, material distribution, thermal history and the opening or release sequence. The visible symptom alone cannot identify which setting should be changed.
Retain the time and location of affected output, especially after a stop or a change in thickness. Do not combine abnormal restart material with steady-running samples when trying to understand the event. After a proposed correction, check the relevant properties rather than treating disappearance of one visible mark as complete verification.
Cool the board for its next operation
Cooling depends on the board, stacking or conveying arrangement and the surrounding conditions. A surface reading and the temperature inside a stack answer different questions. Identify the condition needed for later handling, sanding and measurement instead of using one universal stacking temperature or delay.
Record the board condition used for comparisons. A freshly cooled panel and one that has equilibrated in another environment may differ in dimensions or moisture. The order's acceptance method should identify the appropriate state.
Connect sanding with finished thickness
Sanding should achieve the required finish while retaining the specified thickness. Record the starting condition, material removed and final measurements. Surface damage or a local thickness problem should be investigated before it is assumed that extra sanding will solve it.
For example, if a cooled board measures 18.60 mm and finishing removes 0.25 mm from each face, the nominal arithmetic result is 18.10 mm. These illustrative values are not a recommended allowance. Real acceptance needs measurements across the board and the agreed tolerance, not only a subtraction based on machine settings.
Unequal removal from the faces can alter the supplied construction. Check both surfaces and the relevant density profile when investigating different finishing behaviour. A flat-looking face does not necessarily prove that the board is uniform in thickness.
Choose the supplied size and surface
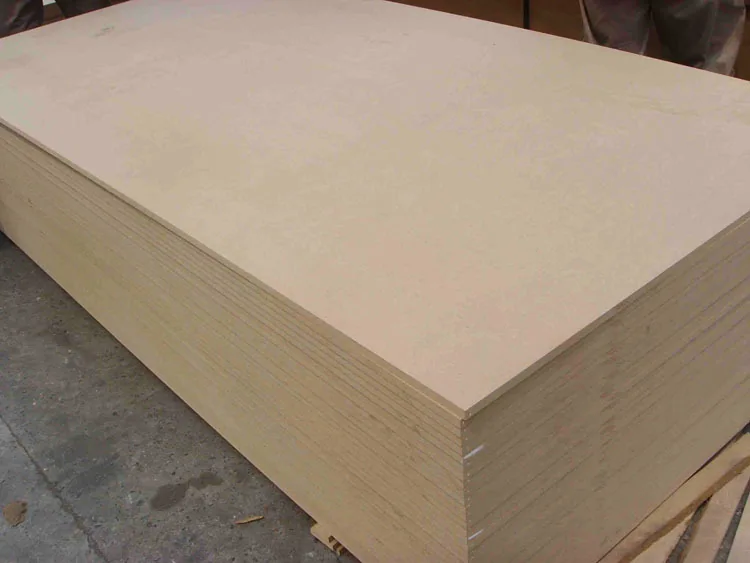
Confirm usable length, width, squareness, edge condition and finished thickness after the relevant operations. Keep trimming allowances separate from the dimensions that the customer can use. Protect the surfaces during transfer so handling damage is not mistaken for a sanding defect.
Specify the next use: painting, veneering, direct decorative-paper lamination or supply as a raw component. These applications can require different surface preparation. Our MDF preparation for melamine facing covers that downstream operation.
Check the properties that matter after a change
EN 310 addresses bending strength and stiffness measurement. These properties remain separate from internal bond, dimensional fit and the surface condition. A process adjustment should be judged against the required set of properties.
Keep the raw observations, specimen identities and relevant acceptance criteria. If a change improves the surface but reduces the required core performance, the result is not resolved. Our MDF quality investigation guide explains how to connect those findings to production records.
Bring the required board condition into your order
Tell us about the part through our enquiry form, with the thickness, sizes or surface reference you already have. We help choose plain MDF or faced furniture MDF and develop the processing, quantity and delivery details. For upstream stages, see the complete MDF manufacturing flow.
MDF pressing and finishing questions
Should I specify a press temperature when ordering MDF?
Usually the useful order details are the finished grade, thickness, surface and component requirements. Our factory manages the production process against that specification; process settings alone do not describe the delivered board.
Why check the routed core as well as the sanded face?
Routing exposes material below the face. Boards with similar average density can have different through-thickness profiles, so trial the actual recess, edge and finishing process.
Is finished thickness measured before or after sanding?
State the supplied stage. For a sanded raw board, agree the thickness after sanding; for a faced or coated part, identify the final measuring stage and its tolerance.