
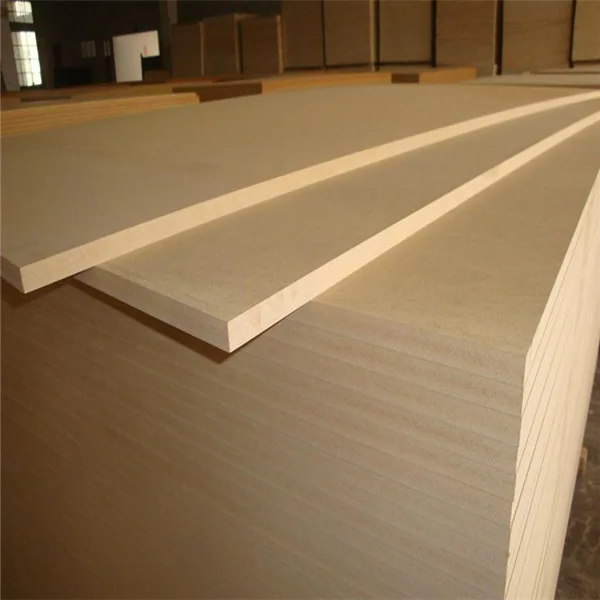
MDF is made by refining wood into fibres, adding binder, forming a mat and pressing it into a board. Cooling, sizing and sanding prepare the surface and dimensions for furniture production. We manufacture MDF substrates in our own factory, then supply plain, faced or processed panels around your project.
For painted fronts, melamine cabinets or veneered interiors, start with the finished look and the work you need done. A photo, sketch or use description helps our team choose the core and develop a sample; the process below explains how those choices connect to the board.
Plain MDF from our factory Furniture melamine MDF Natural veneer MDF
Follow MDF from chips to finished board
The European Panel Federation's manufacturing overview describes the typical sequence of chip preparation, thermal softening, refining, binder addition, drying, forming and pressing. Individual production lines can arrange some operations differently. The important distinction is between making the fibreboard core and subsequently applying a decorative face.
| Stage | Material change | Information carried forward |
|---|---|---|
| Wood preparation | Suitable wood becomes a controlled chip feed | Raw-material identity, condition and contaminants |
| Softening and refining | Chips are separated into fibres | Fibre condition, fines and remaining bundles |
| Binder application and drying | Fibres receive the specified binder system and moisture condition | Material additions, distribution and drying history |
| Mat forming and pre-pressing | Fibres become a transportable mat with controlled mass distribution | Mat weight, uniformity and production position |
| Hot pressing | The mat is consolidated and the binder develops the required bond | Construction, cycle and board identity |
| Cooling and conditioning | The panel approaches the state needed for later processing | Temperature and storage or conditioning history |
| Sizing and sanding | The board reaches its specified dimensions and surface | Finished thickness, surface and usable size |
| Inspection and packing | Verified material is identified and protected for delivery | Grade, lot, quantity and required evidence |
Prepare the wood feed for the selected board
Wood preparation begins with the selected mixture and its condition. Species, chip geometry, bark, degraded material and contamination affect the feed entering the line. These are controlled around the equipment and target board; there is no single wood mixture for all MDF.
Monitor changes in the incoming material and connect them with the affected production period. If chip geometry or moisture changes during a run, the downstream process may receive a different material even though the finished thickness target stays the same. Retain the raw-material reference when investigating a later change in machining or bonding.
Screening and cleaning prepare the feed for the next stage. Their arrangement depends on the installation, while the raw-material and run references connect later machining or bonding results to the board produced.
Refine the chips into usable fibres
Refining changes the wood into a form that can be distributed and bonded as MDF. The resulting material should be assessed for the fibre characteristics relevant to the line, including fines and incompletely separated bundles. A single average fibre length cannot describe the full distribution.
A mill trial on thermomechanical refining examines fibre quality alongside energy consumption. It provides a useful example of assessing the process against more than one response. Its equipment and material conditions do not create a universal refining setting for every MDF plant.
Compare a refining change through the resulting board as well as the fibre sample. Energy use, usable output and required properties belong in the same review, so an attractive fibre appearance alone does not decide the result.
Distribute binder and control drying
Specify the binder and additions with their measurement basis. Liquid adhesive mass, resin solids and dry fibre mass are different quantities. Distribution is also important: a correct overall addition cannot establish that all parts of the fibre stream received the intended treatment.
In some dry-process routes, resin is applied before fibre drying; other systems use a different application arrangement. Record the actual sequence when interpreting a process problem. Drying must prepare the material for forming and pressing while remaining compatible with the binder system.
Keep drying-air temperature, fibre condition and next-stage moisture identified separately. Changes in feed, ambient conditions or residence time affect the material entering forming and pressing, even when the inlet display is unchanged.
Form a mat with controlled material distribution
Mat forming determines how material is distributed along and across the future board. Check the feed and the mass per area rather than relying only on the loose mat's visible height. A uniformly high mat can still contain uneven mass where the fibre condition differs.
Pre-pressing prepares the mat for handling and entry to the main press. Its role should not be confused with completing the board's final cure. Retain any observations of mat disturbance, local damage or loss during transfer because those changes can affect the material entering the hot press.
When thickness and density are specified, connect both to the material quantity. A calculation of density uses mass and volume; it does not reveal how density varies through the thickness or across the board. Our MDF quality-control guide explains those separate questions.
Consolidate the mat in the hot press
A batch press treats a defined charge, while a continuous system carries the mat through a controlled pressing path. The way time, position and process events are recorded therefore differs. Neither equipment description alone establishes the grade or consistency of the finished board.
Record the material combination, thickness, process conditions and output identity. Changing one variable can affect more than one property. The MDF hot-pressing and finishing guide covers pressure and temperature interpretation, density profile, cooling and sanding in greater detail.
Cool, size and sand for the next operation
Cooling, sizing and sanding prepare the panel for its next use. Their order and timing depend on the line and product. Check the actual condition before final dimensional assessment rather than assuming that a fixed waiting period is sufficient for every board thickness and storage arrangement.
Sanding controls surface condition and finished thickness. Specify the resulting surface needed for paint, veneer or direct lamination, and retain adequate thickness for the order. Removing more material is not automatically an improvement: it changes the board that the customer receives.
Cutting establishes the usable sheet size and edge condition. Identify any trim allowance and protect the retained area. A finished panel should be assessed after the operations that determine its supplied dimensions.
Check the finished board against its grade
The official record for GB/T 11718-2021 identifies the current Chinese MDF product standard, replacing the 2009 edition. Where it applies to an order, record the specified grade and relevant evidence. A production-flow description cannot replace product testing or establish every special property.
Keep the required dimensional, mechanical, moisture-related and emission evidence connected to the material supplied. Grade identification, report scope and pack labeling should refer to the same construction. Do not infer moisture or fire performance from board colour alone.
Record the proposed grade, supplied condition and required checks in the document review. Use the document review worksheet.
Choose the MDF and supplied part together
Tell us the furniture or interior use through our enquiry form, with a photo, drawing or sizes you have. We help choose plain MDF, furniture melamine MDF or natural veneer MDF, then develop the processing, sample, quantity and delivery details.
Use the part to plan the supplied MDF. For a painted front, veneered panel or machined furniture part, keep the drawing revision with the chosen stage: sanded sheet, faced sheet, cut blank or machined component. Let the representative sample show the profile, edge, fitting and finish that matter, including work your workshop completes.
Carry the sample and drawing into the grade and supplied-board description. Keep the reports for that configuration and production lot with the order and pack references for receiving checks. Machined and finished samples show the detail reviewed; product reports address the applicable emission, moisture, fire and mechanical requirements.
To keep those production stages connected to the delivered material, use our MDF batch traceability guide. Its split-pack ledger connects production lots, sample reports, shipment quantities and cut-part groups without treating a process description as shipment evidence.
MDF manufacturing and ordering questions
Do you manufacture the MDF substrate?
Yes. We manufacture MDF substrates in our own factory. Choose the board grade and then the plain, melamine or veneer surface and component processing needed for your order.
Is decorative facing part of making the MDF core?
The fibreboard core is produced first. Melamine facing or wood veneer adds a separate decorative construction, with the face, reverse and final thickness specified for the finished panel.
Can I order parts instead of full sheets?
Yes. Start with the parts or sizes you need. We help plan cutting, profiles, holes and the supplied finish, with a representative sample and clear packing identification.